Why Five-Vendor Coordination Fails Before Your Assembly Ever Ships
Splitting a build across vendors creates gaps no single shop owns.
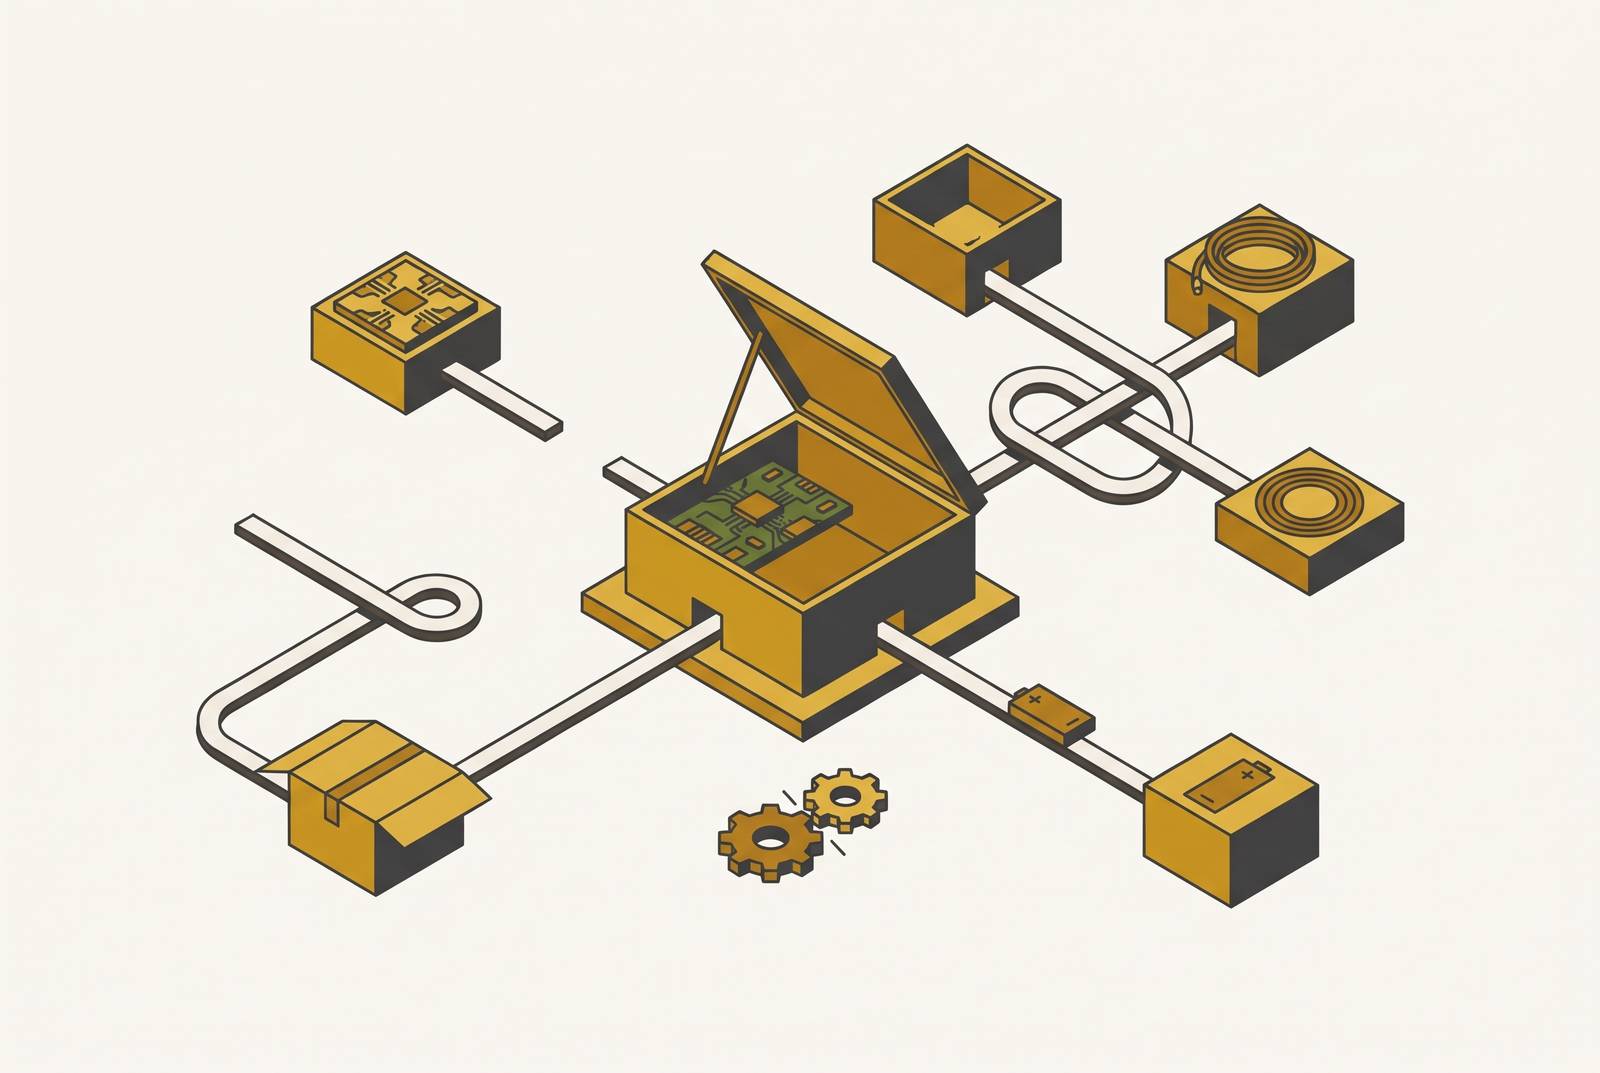
A multi-process mechanical assembly sourcing platform should provide one quote and one accountable partner for machining, welding, finishing, and assembly. Five-vendor coordination fails when each shop commits only to its own work, because the handoffs add delays, split who owns quality, and let designs drift apart. Consolidation addresses that structure only when the partner owns the complete build.
How a five-vendor build is structurally different from a five-vendor risk
An execution failure happens when a vendor misses a deadline or makes a machining error. A structural failure happens when every shop fulfills its own commitment but the assembly still arrives late or fails its requirements. The distinction changes where the problem belongs. Better performance inside each shop cannot, by itself, fix a gap between their responsibilities. The unit being purchased is a complete assembly, while the units being managed are separate jobs.
A team that has shipped a five-vendor assembly on time has shown that the arrangement can work. Success does not remove the underlying exposure. The handoffs remain, and no individual vendor controls what happens on both sides of them. Treating the next build as a test of coordination skill leaves that structure untouched.
Why lead time becomes additive across vendors in ways no schedule can fix
When operations depend on one another, their schedules are serial. A downstream shop cannot begin work on material that has not arrived from the upstream shop. Each independent queue adds waiting time, and movement between facilities adds transit time. Those intervals accumulate along the dependent route. The assembly does not inherit the shortest vendor lead time simply because all the purchase orders were placed together.
A shared schedule can make those dependencies visible. It cannot make them disappear. Each shop still releases work according to its own queue, and the next operation still needs the output of the previous one. Those waits and transfers add to the required processing time. Coordination may track that total closely without giving anyone the power to cut it.
A quality hold makes the dependency especially clear. If one operation stops, every downstream operation waiting for its output stops too. Specialty components create a related choke point. Custom springs, carbon fiber layups, and tube-bent frames can combine extended lead times with single-source exposure, so one unavailable part can delay the entire assembly.
This is not a scheduling problem alone. The hold also raises the question of who owns its cause and resolution across operations. Quality ownership is therefore a parallel problem, present from the start of the build, rather than a downstream concern that begins after the schedule slips.
How quality ownership fractures the moment responsibility is split across shops
Each shop can inspect its own output against its own requirements and accept the result. That does not establish that the outputs will work together. Without someone who owns the assembly, no one owns the interfaces between the shops’ quality systems. A supplier may be responsible for a dimension without being responsible for what that dimension does when combined with the next part. Local compliance is not proof of assembly performance.
A weatherproof enclosure makes the distinction concrete. Its metal shell, gasket surfaces, and internal wiring require coordinated tolerances. Variation across those features can accumulate at the gasket-to-shell interface, even when individual features pass their respective checks. The fit belongs to the assembly. Gasket grooves, seam design, and finishing steps therefore need an owner whose responsibility extends across that interface.
The rating also applies to the whole. NEMA states that an assembly’s overall Type rating is limited by the least severe Type rating of its components. An acceptable shell does not establish that the completed enclosure achieves the required protection. Nor can a finishing inspection stand in for control of the gasket interface. The assembled product must meet its requirements regardless of how many separate inspection reports it has collected.
That requires verification throughout production and at shipment. Incoming inventory, work on assembly lines, and finished batches all need checks under the same quality system. Five independent quality systems do not themselves supply that structure. Without someone in charge across shops, the buyer has to piece together their acceptance decisions and deal with what they leave out.
How revision drift compounds at every handoff until vendors are running different designs
A design change creates another set of handoffs. Every shop touched by the change must get the latest information and use the same revision, even though each has its own tools and processes. Sending a drawing is not the same as establishing a common build definition. When information arrives late or remains inside one department, decisions can rest on incomplete or outdated requirements. More vendors create more places for that break to occur.
The exposure grows over a program’s life. In a new product introduction program, the EVT/DVT/PVT gate sequence gives repeated occasions for design changes to move across the supplier network. A gate alone does not get every shop working to the same revision. If one vendor proceeds with an earlier drawing while another follows the current one, the program is no longer producing one consistent design. The discrepancy can survive until the parts meet.
The bill of materials is part of this control problem. The BOM needs to serve as a risk document at quoting, before it reaches procurement. Each line should have a valid in-production part number, available stock, realistic lead times, compliance status, and at least one approved alternate. Those checks belong inside the BOM tool. That is where the team can act before a questionable component becomes a purchasing commitment.
Revision drift also consumes time already spent. A wrong part has used its place in a vendor’s queue, and rework or replacement starts another wait. At the same time, each shop’s quality system may accept parts based on a different version of the requirements. Additive lead time, fractured ownership, and revision drift therefore reinforce one another, with process interfaces becoming the point where all three meet.
Why DFM breaks down between processes, not within them, in a split-vendor build
Design for manufacturability can be sound for an individual process and incomplete for the assembly. A machining review may establish that a feature is producible without settling how later operations affect its function. The missing review lives between processes. Tolerance interactions, fixturing repeatability, assembly sequencing, and inspection practicality all cross boundaries that a single-process supplier may not own. Without a shared feedback loop, no review closes the whole route.
The distinction is between design correctness and production robustness. CAD and simulation assume geometry, alignment, and repeatability that manufacturing variation does not automatically deliver. Materials, tooling, machines, operators, and time all affect the result. A design can pass a shop’s DFM review and still have problems in production because of those variations. Splitting responsibility makes it harder to connect those variations to the final assembly requirement.
Carbon fiber shows why process choices cannot be deferred to an isolated quote. Fiber grade, resin system, and manufacturing method must be selected before cost can be estimated, and a pilot-run gate is needed before full-scale production. Those choices belong to the manufacturing plan. Treating the carbon fiber part as an ad hoc purchase separates its development from the assembly that depends on it.
Gaskets reveal the same problem from the other direction. Their manufacturability depends on coordinated requirements for the metal shell, gasket surfaces, and internal wiring. A review confined to the seal cannot settle an interface controlled elsewhere. Similarly, bend, weld, and tight-feature choices in sheet metal or tube work affect cost before the finishing vendor receives the formed part. By that handoff, decisions outside the finishing shop’s control have already shaped its input.
Early review can have a large effect on cost because 70–80% of product cost is set during design. But advice only becomes actionable when it is connected to the manufacturing responsibility. The practical file package is a STEP file plus a PDF specifying material, quantity, finishes, and critical tolerances, with tight tolerances reserved for functional features. Good files help communicate intent. They do not replace shared ownership across engineering, manufacturing, quality, and suppliers.
The administrative overhead that makes coordination the hidden cost no vendor quotes
Separate part quotes conceal the work needed to join them into a build. Someone has to line up schedules, pass along design changes, settle questions about acceptance, and keep documents up to date across shops. That effort follows directly from the divided responsibilities. It is not an optional layer added by an overly cautious buyer. When no supplier owns the complete route, the buyer becomes the coordinator by default.
Parts moving between facilities require freight, while separate quality systems can produce duplicated incoming inspection. A quality hold then adds work to expedite parts and get engineers working together on the route that has stopped. Revision drift adds rework or replacement to that burden. None of the individual quotes presents the combined cost of those consequences, so a cheap set of parts can become an expensive assembly.
A missing component from a minor supplier can stop a multi-million-dollar assembly line. Its purchase price says little about that exposure. The work of managing the supplier can also be large relative to the value of the part. Cutting the quoted cost of that item does not necessarily reduce the cost of keeping the build moving.
The cost comparison needs to cover the whole sourcing setup as well as the unit prices. Hardware startup failure rates are near 90%, and process discipline during NPI is cited as one of the main operational causes. That figure warrants closer scrutiny of coordination costs, especially when engineers have little time to spare and fixing handoffs leaves them less time to move the product forward.
How can one vendor quote the whole assembly, and what does consolidation risk?
One partner can quote a complex assembly when its scope covers the required fabrication, finishing, and assembly operations. The structural benefit comes from owning their dependencies. A single commercial front end does not, by itself, provide that ownership if the underlying queues, quality decisions, and revisions remain disconnected. A multi-process mechanical assembly sourcing platform has to be evaluated on who controls the build.
Consolidation removes the external seams where the earlier failures develop. It gives one party responsibility for coordinating operations, accepting the assembly, and controlling design changes across the route. Physical processing time still exists. So do the required sequences and the possibility of defects. Under consolidation, those constraints fall within one accountable scope.
The objection to that concentration is legitimate. With fewer vendors, more depends on the primary partner’s ability to keep running, so the review needs to cover its financial health and disaster recovery plans. Some specialized technical knowledge may also reside in smaller suppliers that the consolidated partner cannot replace. Consolidation has to earn its place through capability and resilience. The number of vendors alone says little about either.
Component-level dual sourcing provides a stronger hedge than rebuilding a parallel five-vendor network. BOM analysis can identify the “golden screws,” namely single-source, long-lead-time, or custom-fabricated parts that concentrate the risk. Pre-qualified alternates for those items protect the assembly while keeping one owner in charge of the whole route. Dual-shore NPI packages can also address geopolitical exposure by qualifying once and ramping where capacity and tariffs favor.
For an engineer evaluating a consolidation partner, the practical checks start with actual scope coverage, including machining, welding, finishing, and assembly where required. Certifications must fit the application. AS9100, for example, applies specifically to aviation, space, and defense. Engineering change order control and traceability complete the test. The partner must be able to keep the whole assembly under one controlled design and one accountable quality system through shipment, which is the problem OneWeekParts, a custom-parts ordering platform that quotes an entire mechanical BOM, hard-to-make parts included, as one order with one PO and one shipment, was built to solve.