What Your RFQ Must Include to Price a Multi-Process Assembly in One Round
Specify each process's minimum inputs upfront to eliminate quote delays and safety-inflated pricing.
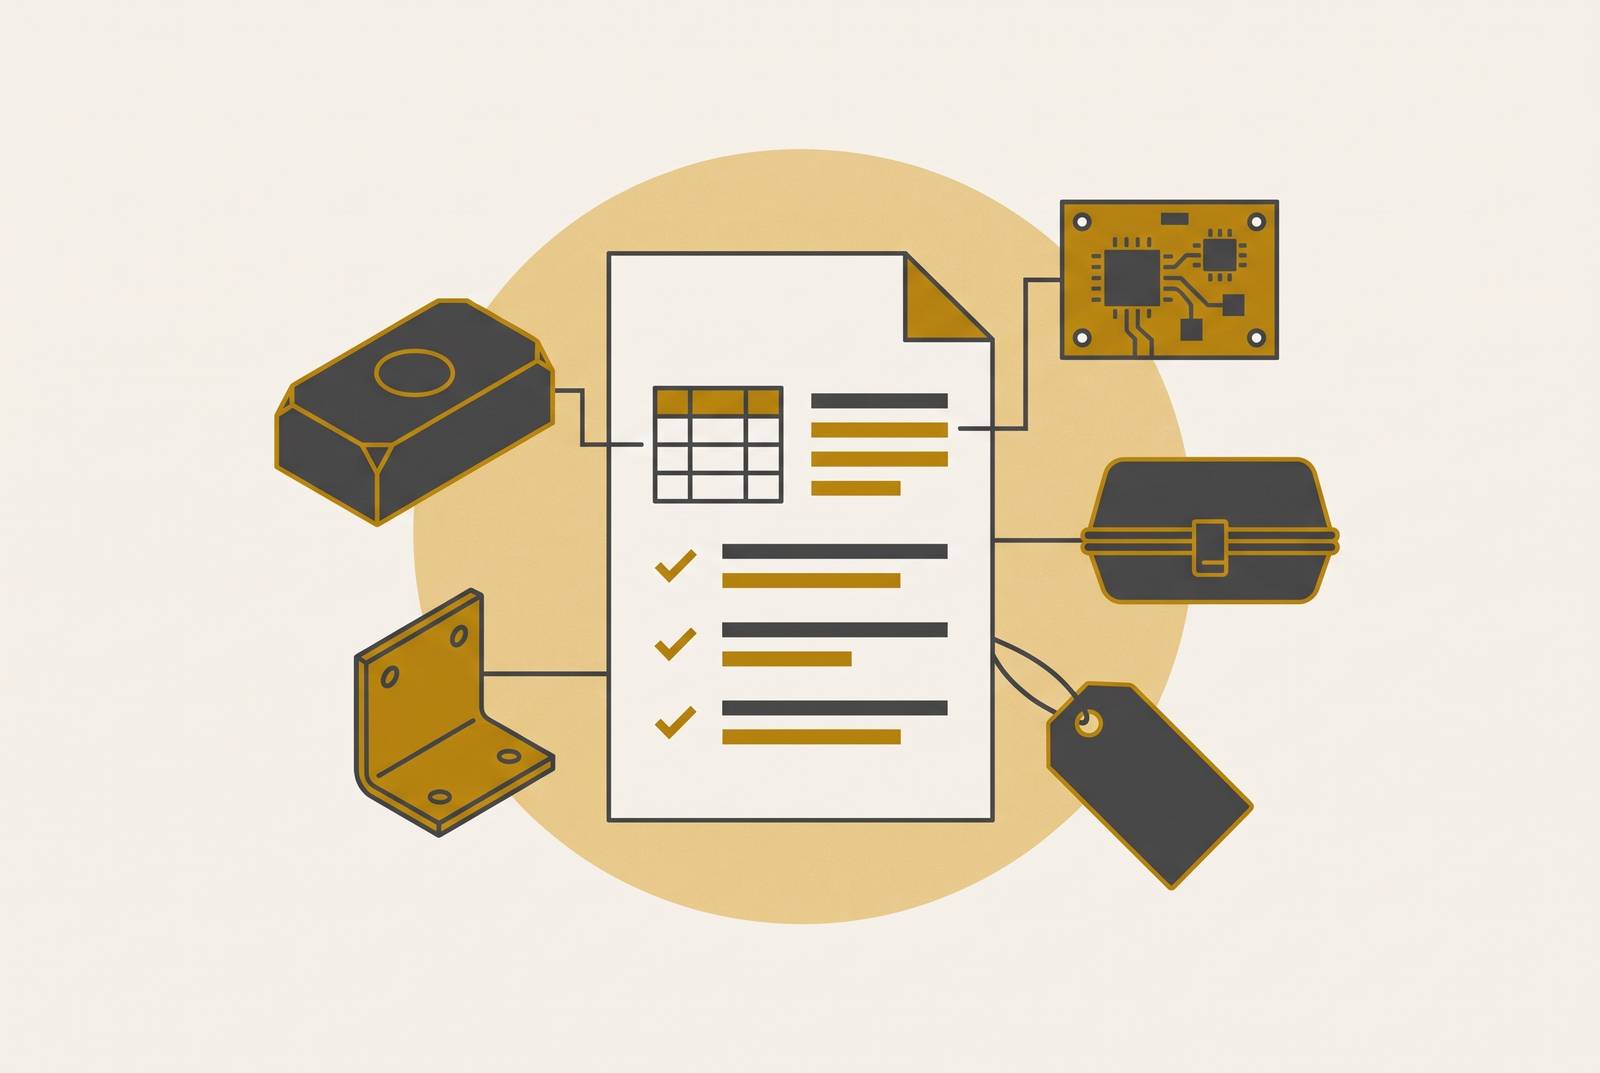
To price a multi-process mechanical assembly in one round, the RFQ must include each process’s minimum inputs and the requirements that bind the BOM together. A multi-process mechanical assembly sourcing platform should check that full package while quoting and collect prices for each part. One missing process input can stall the assembly quote or inflate it with a safety allowance.
Why multi-process assemblies fail to price in one round
A thick RFQ package can still be unquotable. The information an engineer sends must answer the questions each process needs answered. A supplier cannot calculate cycle time, tooling, or material cost from geometry alone when a process-specific input is missing. That gap blocks a complete assembly price even if every other line item is ready.
The supplier then has two ways forward. It can return questions, adding days with each exchange, or assume the worst and price the uncertainty into the quote. The first route delays the buying decision. The second can look like success because a price arrives, but that price includes protection against requirements the supplier cannot yet see.
The file package every process needs before quoting can begin
Check the core package for every part before adding process-specific data. It should contain a neutral-format 3D solid model, a fully dimensioned 2D drawing with a revision level, an exact material grade, target quantity, general tolerance standard, and surface finish requirements. These establish the baseline for quoting. Process-specific requirements add to that foundation rather than replacing it, with a functional spring specification providing an alternative when no formal drawing exists.
STEP is the preferred neutral format for CNC quoting, DFM review, and CAM programming because it preserves precise solid geometry. The export still needs to be usable. If a file has open surfaces or the wrong units, it must be fixed before programming can begin. The drawing serves a different purpose from the model, defining datums, geometric tolerances, threads, and surface requirements that explain how the part will be validated. Its revision must match the model’s revision so the supplier knows which design governs.
Material descriptions also need to be exact. “Steel” does not establish a quotable grade and temper, which affect cost, machining, welding, bending, and finishing. A general tolerance standard such as ISO 2768-m gives the supplier defaults for otherwise unspecified dimensions. Without one, those dimensions remain open questions. Checking this package while quoting lets the supplier spot what is missing before giving a price.
What CNC machined parts need that drawings alone do not communicate
A drawing can be complete enough to describe a machined part without making its function clear. The unresolved feature is often a bearing bore, a datum hole locating a weldment, or a slot holding a gasket. Those features need more than an assumed general tolerance. Highlight or balloon the dimensions that govern fit, mating interfaces, and performance so the supplier can distinguish critical features from cosmetic ones. Tightening every dimension costs more, while leaving functional dimensions at general tolerance raises the risk that parts will be rejected or cause problems during installation.
State the thread form, including UN, metric, or NPT, its class of fit, and whether it is internal or external. A part number alone leaves these questions unresolved. Specify face-specific Ra values on as-machined faces that mate with seals, bearings, or other precision components. Include heat treatment, anodizing Type II or Type III, passivation, and masking requirements before quoting, because vague secondary operations leave suppliers pricing different scopes.
What sheet metal parts need beyond a flat pattern and a bend table
The inside bend radius must be specified against the material thickness and grade. A radius achievable in 5052-H32 aluminum may crack in 6061-T6. That difference belongs in the quoting decision. Otherwise, the supplier must ask questions to settle the bend requirement or add to the price to cover the uncertain result.
Welded assemblies introduce a separate set of requirements. The drawing must show weld type, such as fillet, butt, or spot, together with size and location. Where weld sequence affects distortion or final flatness, note the sequence or add a flatness requirement to govern the result. Fit must also be defined after fabrication. Hole-to-hole location, bracket alignment, and frame squareness can decide whether a part mounts as it should, even when its flat pattern is right.
“Powder coat required” leaves too much open. State the color using a RAL or Pantone code, the gloss level, and masking requirements for threaded holes and mating surfaces. Identify any face that supports a gasket or seal so it is masked before coating. That requirement belongs to both sides of the interface.
What tube bending RFQs must specify to avoid tooling surprises
Specify outside diameter, wall thickness, bend angle, centerline radius, and the distance and rotation between consecutive bends. A 3D model paired with a 2D bending drawing lets the supplier assess manufacturability, tooling fit, and inspection method. Material grade and temper belong in that assessment. They affect wall thinning, springback, and the minimum achievable bend radius, so geometry alone cannot establish whether a tube is producible.
The quote must also cover work after bending. Flared ends, swaged ends, and trimmed lengths each add an operation, while a tube welded to a fitting or frame needs its weld preparation specified. Include both the prototype quantity and the expected production quantity in the first RFQ. Volume and material together shape the tooling strategy, and a one-time prototype may justify a different approach from a production run. Giving both quantities lets the supplier spread tooling cost appropriately and account for the order scaling in the initial quote.
What custom spring RFQs need when no drawing exists yet
A spring quote can go ahead without a formal drawing. Provide wire diameter, outside diameter, free length, end type, material, and quantity, plus load at working height for a compression spring or torque at working angle for a torsion spring. Photos of a reference part and those dimensions can form a workable package. If a drawing exists, send it as PDF, DWG, DXF, or STEP. The supplier’s engineering review can then find what is missing before quoting.
The required load is only the starting point. Custom springs typically need a 15–20% force margin for fatigue and temperature variation, so state the working load and allow the supplier to design in a margin, or specify it explicitly. Describe the operating environment because carbon steel, higher-alloy stainless grades, and superalloys involve large cost differences. Include any required number of full-stroke cycles and life testing before shipment. Also explain what the spring compresses against, whether it is dynamically cycled or statically loaded, and what it interfaces with so end-type or formed-feature problems can surface before tooling is cut.
What gaskets and sealing faces need specified to prevent a fitment failure
A gasket can pass inspection and still leak. Its standalone dimensions do not establish whether it will seal against the mating surface under operating conditions. The RFQ must link three requirements that are often left out: mating surface finish, compression set requirements, and compatibility with the operating fluid or gas.
For a machined flange, specify its Ra value on the machined part drawing and cross-reference it in the gasket RFQ. Gasket hardness and flange finish must work together. If the mating face is on a powder-coated component, cross-reference the masking requirement established in the sheet metal package. State the operating fluid or gas, temperature range, and pressure so material selection can distinguish between neoprene, EPDM, PTFE, or a metallic spiral wound gasket.
Bolted joints need their own load information. Provide the bolt pattern, bolt load, and expected compression so the supplier can assess sealing without extrusion or permanent set under the clamp force. The dimensional minimum is ID, OD, hole pattern, and thickness. Where the gasket also orients a fitting or locates a port, its positional tolerances must reflect both its outline and that assembly function.
How BOM-level information completes the picture that individual part drawings cannot
For the whole assembly, the BOM must set out the quantity strategy, the rules for substitutes, the order of deliveries, and the quality documentation needed. State the prototype quantity needed now, any first article quantity, the expected production run quantity, and the estimated annual usage. These stages can have different cost structures. A budgetary estimate and a production-ready quotation are not interchangeable, so the requested quote must make its intended basis clear.
Substitution rules must be explicit at this level. State whether substitutes are banned, are pre-approved, or need written engineering approval before use. A matching description or envelope does not establish equivalence when grade, temper, finish, or tolerance affects function. Define assembly operations with the same care. Pressed bearings, bonded seals, staked inserts, and conformal-coated surfaces must be listed with acceptance criteria so the supplier knows this work is part of the order.
“Fully tested” does not say which checks will be performed, what equipment or fixture will be used, under what conditions, or against which pass/fail limits. Spell out each of these details so suppliers quote the same acceptance work. Then name the inspection level, whether visual, CMM spot-check, or full critical dimension inspection, together with the first article inspection report format. Include required mill certs and material test reports because documentation and inspection labor are not included by default.
Traceability needs a defined depth. If the assembly must be traceable to material lots, build revision, process records, or approved deviations, say so before the purchase order. A serial number without retrievable history does not provide that traceability. The required record cannot be retrofitted after production begins.
How DFM feedback built into quoting prevents second rounds before they start
A complete specification can still describe an impractical part. Design for manufacturing review, or DFM, catches a different class of problem from missing information. A tolerance may be stated correctly but unachievable for the process, or a fully defined bend may need a non-standard die. A gasket groove can likewise be fully dimensioned yet too small for the sealing material’s compression range. These are reasons to review the design while pricing it.
During quoting, feedback can settle a question within the original quote cycle. After the design is frozen and tooling committed, the same finding becomes an engineering change with cost and schedule consequences. The lesson for engineers is to look for a sourcing partner that provides instant DFM feedback within quoting and assigns same-day engineering support. An optional pre-production review comes too late to prevent the quote from resting on an unresolved design.
With one quote, one purchase order, and one shipment, the same engineering team can see the full BOM. That makes it better positioned to review the connections between machining, welding, finishing, and sealing. For a buyer seeking one vendor for a mixed-process assembly, a useful distinction is whether the vendor’s quoting process resolves requirements between parts before turning them into a single price.