Grading Prototype Sourcing Platforms on the Lines They Refuse to Quote
Quote refusals reveal what sourcing platforms can really handle.
Full BOM sourcing for mechanical prototypes requires a partner that can quote the hardest custom parts and off-the-shelf lines together. An evaluation of sourcing platforms considers what they decline, what they explain, and what they send to engineering review.
Why refused quotes are the most honest signal a sourcing platform gives you
An engineer simplifying geometry during concept validation just to clear a quoting engine is solving the platform’s problem. A manufacturable pocket or undercut can disappear from a design because the software cannot price it. The engineer then tests a version that fits the quoting rules in place of the concept they meant to test.
A refusal is therefore a capability disclosure. It can mean the platform cannot make the part, but it can also mean its algorithm cannot price it. Those are different limits, and a generic rejection hides the distinction. Engineers often find this out only after they have prepared files, chosen processes, and set up an account. The time has already been spent when the platform finally reveals where its service stops.
How automated quoting engines decide what they will and will not touch
Instant-quote engines work well with simple geometry and standard tolerances because they already have rules for pricing those jobs. The engine reads a STEP file, recognizes features, and checks them against an acceptance envelope. That envelope is the range it can handle. Features outside it may trigger a decline or a handoff to manual review, even when a skilled machinist could make them.
An engine that reads only a STEP file cannot read GD&T callouts on a separate drawing or judge whether the chosen process will make the part work as required. Certain internal radii, complex pockets, and undercuts requiring repositioning can demand production planning beyond its rules. Tight tolerances, 5-axis geometry, deep cavities, special materials, and demanding finishes make that gap more pronounced.
An engine may refuse a quote or build uncertainty into the price, leaving the engineer with a figure that is unreliable for planning. Both outcomes come from the same missing step, which is a workable production route. Accepting the file alone does not show that this step happened.
What the refusal pattern actually grades: the five dimensions that matter
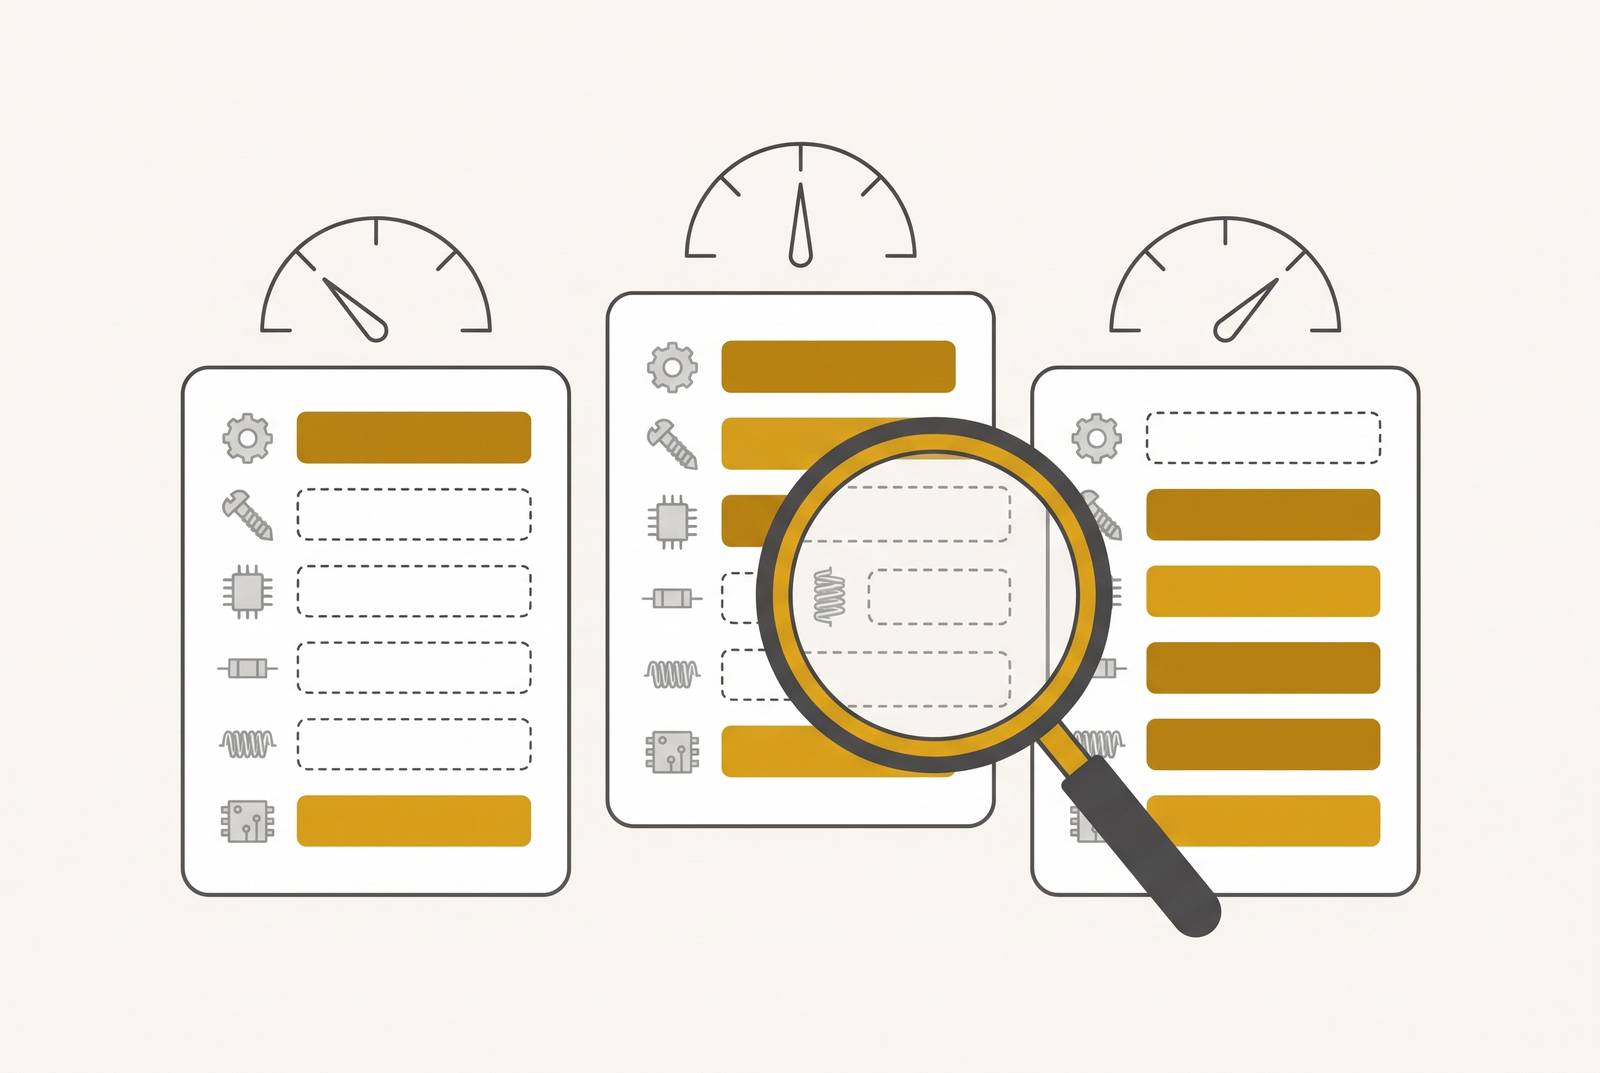
The first dimension is the geometric acceptance envelope. A platform earns a stronger grade when it distinguishes a genuinely unworkable feature from one that merely needs a different setup. Rejecting both forces design compromises for the wrong reason. The second dimension is process coverage, specifically how fully the quoting engine can price the processes listed on the website.
The third dimension is how the service handles a multi-process BOM. A bill of materials that includes CNC, sheet metal, casting, and specialty fabrication tests whether the service can give one usable quote or just separate prices. Coordination belongs in that assessment because supplier handoffs add queue time, freight, and quality-dispute risk. A fast price on one line says little about the procurement effort for the assembly.
The fourth dimension is refusal transparency. A specific explanation about geometry, tolerance, or material gives the engineer something to resolve, while a generic failure provides no useful direction. The fifth is the inverse failure mode, namely accepting everything without meaningful review. These are qualitative grades. A platform earns a better grade by checking what it accepts and refuses than by just giving more quotes.
Platforms graded: where the geometric acceptance envelope is too narrow
Automated quoting platforms are a strong fit for standard parts when speed and repeatable pricing are the main needs. Their DFM checks can flag thin walls, deep pockets, and problems with the internal-radius before the part is made. The weakness appears when the same boundary treats a difficult but manufacturable feature as though it were a design error.
This class gets a mixed grade for prototypes that are hard to make. Its speed remains useful on straightforward lines, but its acceptance envelope can exclude precisely the parts that need the most planning. For a complex BOM, the service then gives only part of the answer: it prices standard parts and turns down difficult parts or holds them for review.
The decisive distinction is what follows the flag. Specific DFM feedback can reveal a real constraint, while engineering review can establish whether another setup or production route makes the feature feasible. Without either, the platform offers little help beyond the boundary of its rules. Its fit is narrower than its upload workflow suggests.
Platforms graded: where process coverage is narrower than advertised
A listed process is not necessarily an instantly quotable process. For tube bending, automated support may cover round profiles and rotary draw bending but leave out rectangular tubing or complex multi-plane geometry. OSH Cut’s CNC tube bending page identifies round profiles as its current tooling scope and offers in-browser DFM checks.
Outside that scope, a one-off bend can require days or weeks of discussion about CLR constraints, springback, and fixturing. A platform can legitimately offer tube bending while still needing manual intervention for a particular part. Its grade depends on whether that boundary is visible before the engineer invests time in submission.
CarbonVega and uMake are specialist options for instant quoting of cut carbon fiber sheet parts. A finished composite part may require engineering review, material selection, tooling, layup or forming, consolidation and curing, demolding, trimming, finishing, and inspection. Choosing that route depends on geometry, load direction, quantity, tolerance, and surface requirements, so sheet-cutting support does not establish broader composite capability.
Cast urethane exposes a similar input problem. A STEP file and quantity do not establish Shore hardness, master pattern ownership, cosmetic requirements, or insert specifications. Those details affect the cost of the job. A service that collects them through review may be capable, but a generic upload form cannot support an accurate price by itself.
How do you source every part on a mechanical prototype BOM without using five vendors?
Cutting, bending, welding, and finishing may each run quickly, yet moving work between suppliers adds queues, freight, and inspection cycles. The assembly waits for the handoffs as well as the operations. The speed of a quote for each part tells only part of the story of total lead time.
Fragmentation also divides responsibility for defects. If a problem in a finished assembly could have originated at any of several upstream suppliers, no single vendor owns the whole corrective action. The engineer must work through differences in the inspection reports and get the suppliers to work together on a response. That work consumes engineering time during an already unsettled prototype cycle.
Supplier-network marketplaces give buyers access to shops with a range of skills, but buyers still need to know who makes each part. When the buyer does not know the producing shop, traceability and repeat-order consistency become harder to manage. A broad network also gives no assurance that specialty lines and purchased parts will be in the same quote as standard machined components.
For full BOM sourcing, the relevant distinction is consolidation. A service that prices only the straightforward lines leaves the buyer to finish the sourcing job. A partner that can quote CNC, sheet metal, carbon fiber, custom springs, tube bending, casting, and assembly in one transaction addresses the coordination gap. Whether off-the-shelf parts are included must also be established.
Platforms graded: the inverse failure mode of accepting everything without review
A platform that accepts every upload may simply move the discovery of a problem from quoting to production. That is a much worse place to find it. Turning down a design before tooling avoids costs that can grow into weeks of delay and large bills once tooling or first-article production has begun.
Services that do little review are thus a poor fit for jobs where function and tolerance need a close look. A quoted part can still fail its intended use, with especially serious risks in industrial, aerospace, or medical applications. A clean checkout is not an engineering judgment. The absence of a refusal is useful only if someone or something has meaningfully checked the design.
CoLab’s AutoReview illustrates what a defined first-pass check can cover. It performs deterministic geometric checks for CNC machining, injection molding, and sheet metal, including hole depth-to-diameter ratios, internal radii, thin walls, wall thickness uniformity, draft angles, and bend radii. These checks help with review, but engineering judgment is still needed. A response such as “this internal radius is below the minimum tool diameter for the specified process” gives the engineer an actionable constraint.
A design flaw added on purpose is a useful way to test the service before sending a full BOM. Specific annotation shows that the system recognized the problem. An unexplained acceptance or generic refusal does not. The strongest grade goes to a service that explains genuine limits and escalates resolvable complexity instead of treating every file as either automatically acceptable or impossible.
Human review as the design decision that separates a refusal from a capability
An engineer can assess multi-axis components, undercuts, and tight-tolerance assemblies in terms of how they could be made. That assessment makes the refusal a manufacturing decision.
The trade-off is time at the quoting stage. Complex parts typically require a business day or more for human review, which is slower than an instant result. That delay must be weighed against a declined line or an unreliable price.
The Spring Store offers a narrower example of automation grounded in a specific process. Its Spring Creator X calculates spring rate, maximum safe travel, and solid height, while warning about buckling risks and solid height limits. Parts that are more complex than standard geometry go to human review. The useful design principle is to automate what can be priced accurately and escalate what needs judgment.
Drawings make the advantage of that judgment especially clear. An engineer can read a PDF drawing with full GD&T and notes as the contractual specification, while a STEP-only workflow may miss requirements absent from the model. The recommended submission includes both documents. AP214 supports broad STEP compatibility, while AP242 can provide embedded PMI if the supplier supports it, and the PDF preserves the specification for review.
What engineers should ask before uploading a file to any sourcing platform
Qualifying the service starts with the hardest BOM lines. Which parts need 5-axis machining, tight tolerances, tube bending, carbon fiber, cast urethane, custom springs, or cross-process assembly work? Those lines expose the real boundary. Standard machined blocks are unlikely to show whether the platform can handle the whole program.
Ask which listed processes receive automatic quotes and which require manual review, including the realistic turnaround for each. Then ask whether the service will quote the complete BOM in one transaction, including custom parts and off-the-shelf items. Same-day engineering support is a useful distinction when unresolved lines would otherwise send the team back to separate suppliers.
Before preparing the files, confirm that the receiving workflow uses both the model and the drawing. A STEP-only submission can omit GD&T requirements supplied separately, while a PDF-only submission can force the shop to model the part from scratch. Test the DFM response with a known flaw as well. The useful result identifies the problem.
Finally, ask what happens when a line cannot be quoted automatically. Does the response name the geometry, tolerance, or material constraint, and can an engineer assess another production route? That answer separates a useful boundary from a dead end. For a complex prototype BOM, the strongest sourcing partner is the one whose process does not stop when the instant quote does.